The SigmaCapSeal 440M is a fully automatic precut Liner/Wad inserting machine designed for accurately inserting EP, Foam and Induction Liners/Wads into plastic caps and closures.
Using a proven vacuum Pick & Place system, the machine inserts one precut liner into every cap at speeds of up to 160–180 caps per minute, ensuring consistent liner placement with high reliability and minimal operator intervention.
Automatic EP, Foam & Induction Wad/Liner Insertion for 20-50 mm Caps
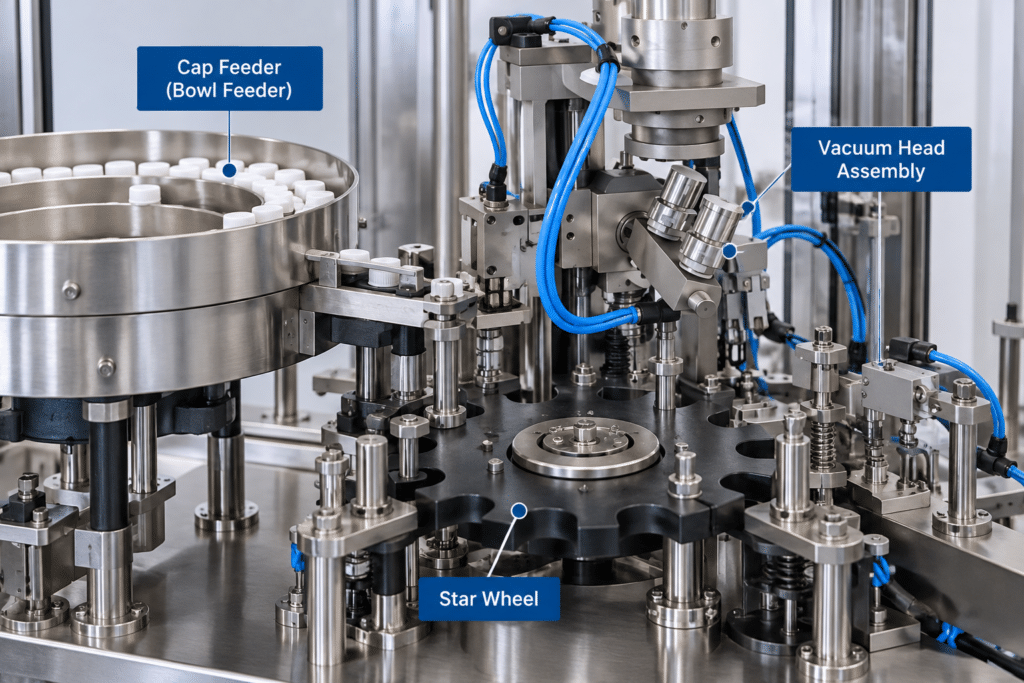
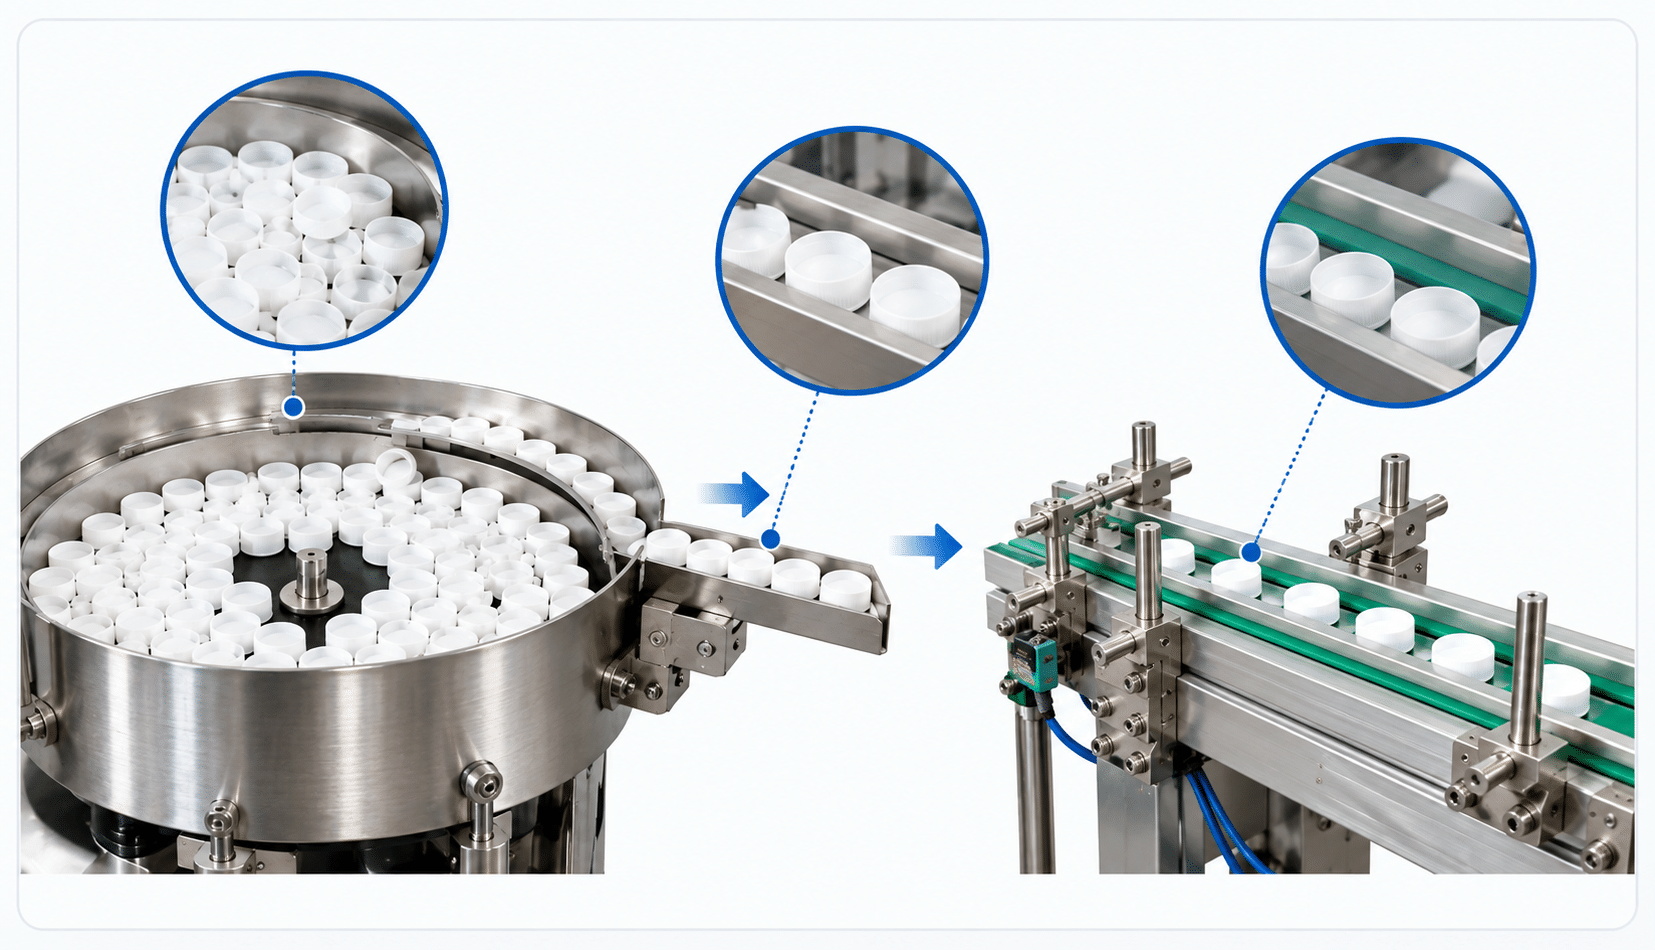
The 440M automatically inserts precut induction/EP/Foam wads into 20-50 mm caps. Caps are fed into a bowl feeder and oriented cavity-facing up, then carried by conveyor to a star wheel that holds each cap in position while a vacuum cup places a wad from the magazine into it.
The sensor arrangement catches a missing or flipped wad in the same motion that places a good one: no-wad and reverse-wad rejection runs through a camera vision system, with a rejected cap counter and an accepted cap counter tracking output. The whole line is PLC controlled from a 7-inch touch screen operator panel.
Four stations, one continuous motion. Caps get oriented, wads are stacked and ready, the star wheel brings the two together, and the vacuum cup does the placing.
1
Cap Feeding and Orientation
Caps load into the bowl feeder and come out cavity-facing up, delivered by conveying belt toward the wadding station. A cap orientation validator sensor blows wrongly oriented caps back to the hopper.
2
Wad Magazine Stacking
Precut induction/EP/Foam wads sit stacked in the magazine, aluminum-facing down, staged and ready for the vacuum cup to draw from one at a time.
3
Star Wheel Indexing
A star wheel holds each cap in position as it indexes toward the wadding station, keeping placement repeatable at 160 to 180 CPM.
4
Vacuum Pick-and-Place
Each time the star wheel indexes, the vacuum cup lifts one wad off the magazine stack and sets it into the cap. No-wad and reverse-wad rejection with a camera vision system checks the result before the cap moves on.
Watch the 440M in Action
440M Spec Sheet
The full brochure PDF with dimensions, head options and accessory list, ready to forward to your engineering or procurement team.
A star wheel and vacuum cup place a precut induction/EP/Foam wad from the magazine into every 20-50 mm cap.
Stainless Steel Bowl Feeder
Main bowl structure in stainless steel AISI 304 on an M S painted stand, with a quick-change cap sorter and an acrylic cover for dust-free operation.
Cap Orientation Validation
A cap orientation validator sensor checks each cap is cavity-facing up after the bowl feeder; wrongly oriented caps are automatically blown back to the hopper.
PLC Control with Touch Screen HMI
Programmable PLC (Mitsubishi / Panasonic) with a 7-inch color touch screen operator panel and a three-color alarm light.
160 to 180 CPM, Rated
Caps are fed, oriented, wadded and counted continuously at up to 180 caps per minute.
Automatic Box-Fill with Alarm Light
The exit conveyor’s two-position switch gate and cap counter fill boxes to your set quantity, with an alarm light prompting the operator to swap to the second box once the first is full.
A cap orientation validator, a reverse cap sensor, and camera-vision no-wad/reverse-wad rejection watch the cap and wad through the cycle, with rejected and accepted caps each counted.
No Wad / Reverse Wad Rejection
A camera vision system checks for a missing wad or a wad seated the wrong way up.
Reverse Cap Sensor
Positioned on the entry conveyor near the star wheel; stops the machine if a cap arrives the wrong way round.
Rejected Cap Counter
A rejected cap sensor with counter tracks every cap that fails the wadding or orientation check.
Accepted Cap Counter
Running count of every cap that passes through the station successfully.
Cap Level Sensors
Level sensors on the cap elevator and at the entry and exit of the infeed conveyor start and stop the elevator, bowl feeder and wadding process as caps run high or low.
Construction
Mechanical, pneumatic and electrical build, per ED engineering drawings.
Mechanical
Parts exposed to wear are standard, from international suppliers
Parts not in stainless steel have corrosion-resistant coating or customer-specified paint
Every part manufactured to its own drawing, per ED engineering
Pneumatic
Festo / SMC make, per ED engineering
Electrical & Control
Electrical cabinet per CEE electrical security directives
PLC: Mitsubishi / Panasonic, programmable type (24VDC PNP)
Operator panel: Mitsubishi 7-inch color touch screen
Marked cables and connectored modules; inverters standard; Bonfiglioli gear box
The infeed system ships as standard, built for dust-free operation end to end. One item is available on request but not included in the standard provision.
Standard Infeed System
Cap elevator to bowl orientor, dust-free enclosed path
Dual-track infeed conveyor with inverted cap removal at machine entry
Adjustable guides for cap diameter, height and width
Exit conveyor with counter and diverter
Optional: Camera Inspection System
Not included in the standard infeed provision
Adds a camera-based check at the infeed/exit conveyor
Every stage of the cap and wad path is monitored, and the machine is guarded to stop on demand or on fault.
Sensor / Device
Location
Function
Cap Level Sensor
Cap elevator
Alarms and controls elevator level
Cap Level Sensor
Entry of infeed conveyor
Starts / stops the cap elevator motor
Cap Level Sensor
Entry and exit of infeed conveyor
High level stops the bowl feeder; low level stops the wad inserting process
Reverse Cap Sensor
Entry conveyor, near the star wheel
Stops the machine on a reversed cap
Cap Sensing
Entry of the star wheel
Confirms cap presence before indexing
No Wad / Reverse Wad Rejection
Wadding station (camera vision system)
Rejects caps with a missing or reversed wad
Rejected Cap Sensor with Counter
Exit
Counts rejected caps
Accepted Cap Counter
Exit
Counts accepted caps
Touch Sensor
Clutch mechanism
Safety stop
Door Safety Sensors
Guarding doors
Safety stop
Start / Stop / Emergency Button
Control cabinet
Manual start, stop and emergency stop
The equipment stops automatically under any of the above conditions. Security perimeter closure with hinged doors is fitted around the machine.
Cap Specification, Wads and Industries
What the 440M is built to run, and where it’s used.
Cap Specification
Cap size: 20-50 mm
Cavity-facing-up orientation
Wrongly oriented caps auto-rejected back to hopper
Wads
Precut induction/EP/Foam wads
Stacked aluminum-facing-down in magazine
Where It's Used
Pharmaceutical and healthcare packaging
Food and beverage bottling
Personal care and cosmetics
FMCG production lines
Agrochemical, specialty chemical and lubricant fills
Industries Running the 440M
The 440M is built for manufacturers of plastic caps and closures needing automatic insertion of precut EP, Foam or Induction liners/wads — widely used across pharmaceutical, food, beverage, chemical, lubricant and agrochemical production, where consistent liner placement and high product quality are essential.
Pharma & Healthcare
EP, Foam and Induction liner insertion checked by vision inspection before the cap moves on.
Food & Beverages
EP, Foam and Induction liner insertion at up to 180 caps per minute.
Personal Care
Consistent liner placement for 20-50 mm caps.
Agro & Specialty Chemicals
Reliable liner insertion for chemical container closures.
FMCG
High-volume liner insertion built into fast-moving consumer goods packaging lines.
Pharma
Precise EP, Foam and Induction liner placement for pharmaceutical closures, inspected on every cycle.
Specialty Chemicals & Lube Oil
Dust-free liner seating for specialty chemical and lubricant container closures.
Sigma CapSeal designs and builds the full closure line — wad/liner insertion, cap assembly, induction sealing and vision inspection — so every station on your line is specified, quoted and serviced by the same applications team.
Sigma CapSeal has built wad/liner insertion, cap assembly, induction sealing and vision inspection equipment since 1974 and shipped India and Asia’s first induction sealer in 1989. That’s the same engineering group behind the 440M’s feed, index and placement mechanism, backed by a DSIR-certified R and D lab and equipment running in more than 85 countries.
What packaging engineers, procurement teams and QA managers ask before they buy.
How does the 440M insert liners into caps?
Caps are loaded into the hopper and transferred by a cap elevator to a bowl orientor, which orients them before they discharge onto the conveyor. A precision star wheel indexing system positions four caps at a time beneath a vacuum Pick & Place head, which lifts a precut EP, Foam or Induction liner from the magazine and places it into each cap. A Liner Presence/Absence Detection System then inspects every cap and automatically rejects any without a liner.
How fast does the 440M run?
160 to 180 caps per minute.
How does it catch a missing or misoriented cap or wad?
A cap orientation validator sensor blows wrongly oriented caps back to the hopper. A reverse cap sensor stops the machine near the star wheel. A Liner Presence/Absence Detection System automatically rejects any cap without a liner, with a rejected cap counter and an accepted cap counter tracking output.
What cap size and liner type does it handle?
20-50 mm caps, with precut EP, Foam and Induction liners/wads.
Is the 440M PLC controlled?
Yes, on a programmable PLC (Mitsubishi or Panasonic) with a 7-inch color touch screen operator panel.
What's the power requirement?
220/380/440V AC, 50/60Hz+N+T, with an auxiliary control voltage of 24V DC. Rated for 5 to 40 degrees C and 20 to 85 percent relative humidity.
Spec a 440 M for Your Line
Send us a cap sample for inspection. Our applications team will confirm the scope of supply before you commit.