FTC-100 Automatic Flip Top Cap Folding Machine — Oval Cap
Purpose-built folding for oval and other non-round flip top caps, from the feed bowl to the collection box.
A flip top cap is a single molded piece with a built-in hinge, fed into the machine already open. Not two components to join, one hinge to close and lock. Most folding machines are built for round caps and adapted, not designed, for oval ones. The FTC-100 is set up around the oval’s long and short axis from the start: SS 304 bowl tooling, star wheel pockets and the folding guiding system all match the shape, so caps fold and lock consistently instead of skewing off-center.
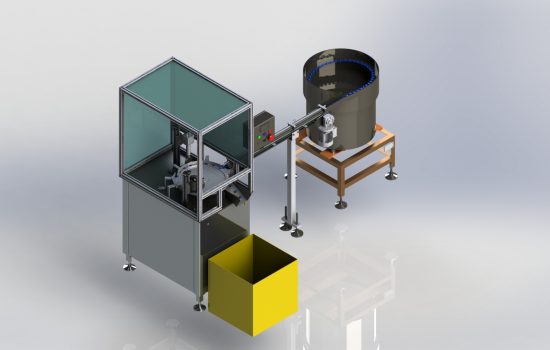
A flip top cap is molded as a single piece with a built-in hinge. It arrives from the injection molding line already open, and the FTC-100’s job is to close and lock that hinge, not join two separate cap components. It feeds the caps, orients them, softens the hinge, closes it against a stationary folding guiding system, then locks it so it holds.
For oval caps specifically, the machine also has to keep the cap oriented along its long axis the whole way through, since an oval will not sit or index the way a round cap does. That is the part most folding machines get wrong when they are built generically for “flip top caps” without accounting for the shape.
An oval cap has a long axis and a short axis, and if it enters the folding station rotated even a few degrees off, the fold comes out uneven. Three parts of the machine have to be built around that shape specifically.
1
SS 304 vibratory bowl tooling
The bowl track has to filter and orient caps so only correctly-aligned ovals move forward. Wrong tooling here causes jams or caps entering sideways.
2
Star wheel pockets
These have to match the oval’s exact profile, not a generic round pocket with clearance, or the cap will shift mid-index.
3
Folding guiding system placement
The stationary guiding system has to be positioned to match the oval’s fold line, usually along the short axis, so the fold happens at the right point as the cap rotates past.
Get any of those three wrong and it shows up in the reject bin: skewed folds, cracked hinges, caps that pop back open.
How the FTC-100 Folds a Cap
1
Vibratory Bowl Feeding & Orientation
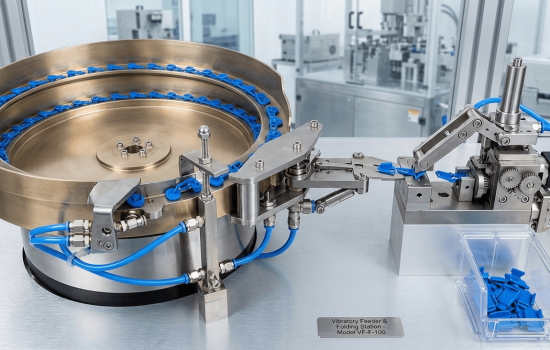
Caps are dumped into the SS 304 vibratory bowl feeder in bulk. The bowl track orients each cap consistently in a single track, then rejects anything sitting wrong.
2
Feeding Conveyor Transfer
Correctly oriented caps move from the bowl onto the feeding conveyor, which carries them to the folding station in a steady, single-file line.
3
Rotary Star Wheel Indexing
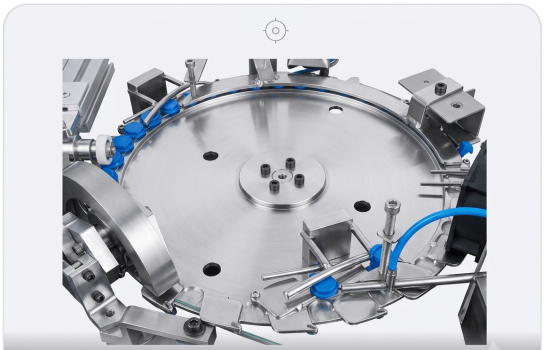
The conveyor feeds caps into a rotary star wheel, which picks each one up into its pocket and indexes it forward at a fixed rate, keeping spacing and orientation consistent.
4
Hinge Softening (Hot Air Heater)
After the cap enters the star wheel pocket, it passes below a hot air heater/blower that softens the hinge, so it folds and closes without cracking.
5
Folding via Folding Guiding System
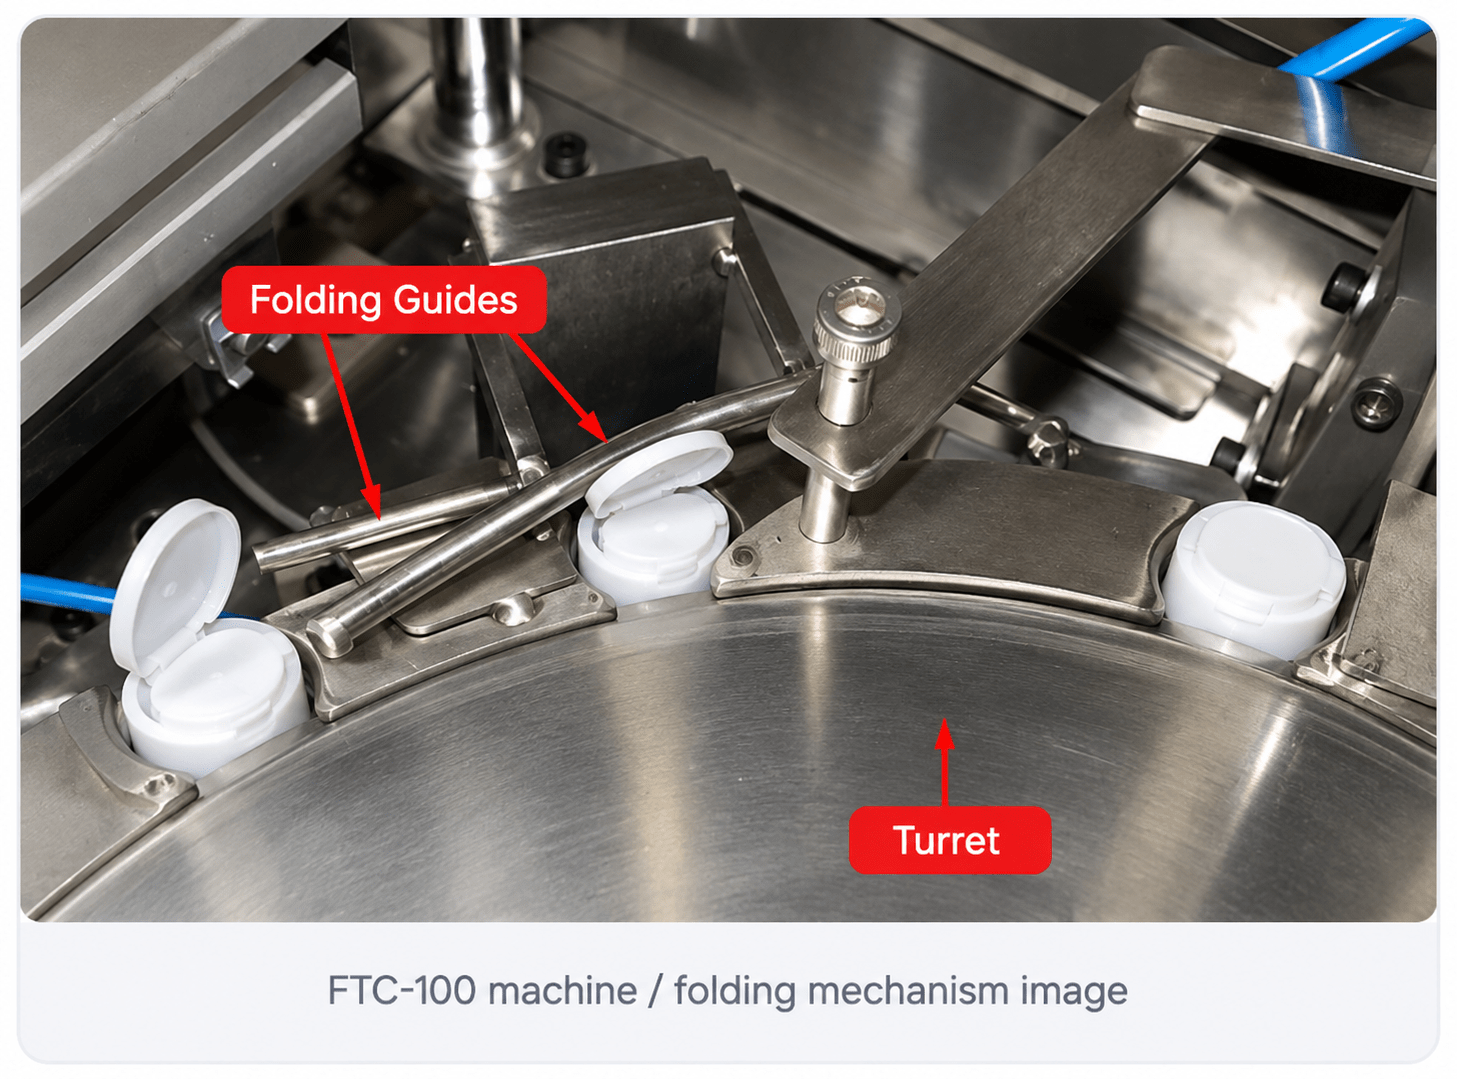
The cap stays in its star wheel pocket, moving in continuous rotary motion. The softened outer flip closes on contact with a stationary folding guiding system as the cap rotates past it, not a cam.
6
Silicon Roller Closes & Locks the Flip
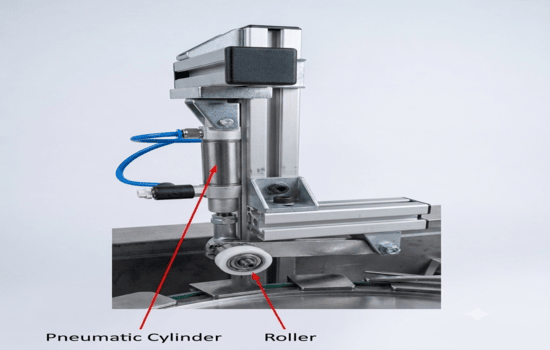
After the folding guiding system closes the flip, the cap passes through a silicon-based roller, which closes and locks the flip.
7
Pneumatic Cylinder Final Press & Hinge Lock
A pneumatic cylinder gives the flip a final press and locks the hinge, while the cap continues in rotary motion.
8
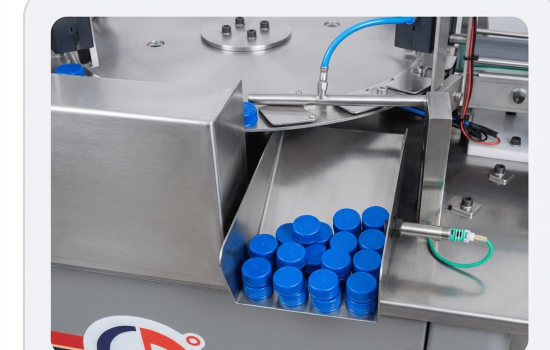
Ejection & Collection
The folded, locked cap moves off the star wheel and gets ejected into the collecting box, ready for the next stage of your line. An optional diverter can route rejected caps separately.
Why Choose the FTC-100
The capabilities that make the FTC-100 a dependable oval-cap folding line.
Oval-Specific Orientation Tooling
Bowl track, star wheel pockets and folding guiding system placement are set up for oval geometry, not adapted from a round-cap machine.
Any Cap Shape or Size
Tooling is custom-matched to your cap’s exact profile, whether oval, round or another shape, instead of locking you into one fixed diameter range.
Hinge Softening Before Folding
A hot air heater softens the hinge in the star wheel pocket before folding starts, so the fold closes cleanly instead of cracking.
Stationary Folding Guiding System
The cap moves in continuous rotary motion in its star wheel pocket; the flip closes on contact with a stationary guiding system, not a cam.
PLC + Touch-Screen HMI
Set speed, monitor cycle counts and adjust timing from one control panel.
SS 304 Cap-Contact Parts
The vibratory bowl feeder, cap guiding system and other cap-contact parts are SS 304, hygiene-grade construction suited to cosmetics, personal care, pharma and food packaging lines.
Vision Inspection Ready (Optional)
Optional add-on, at additional cost, that checks fold completeness and rejects bad caps before they reach the collection box.
Diverter Mechanism (Optional)
Not standard equipment. Available at additional cost, the diverter routes rejected or incomplete caps away from the main collection line for separate handling.
Guiding-System-Driven vs. Servo-Driven Folding
Both fold caps correctly when set up right. The difference shows up in changeover and precision.
Factor
Guiding-System-Driven
Servo-Driven
Setup cost
Lower
Higher
Changeover between cap sizes
Physical guide/tooling swap
Recipe-based, faster
Fold precision on tight tolerances
Good
Tighter, with real-time feedback
Maintenance
Simpler, fewer electronic parts
Requires servo/drive expertise
Best fit
Single cap size, high volume
Multiple cap sizes on one line
The FTC-100 runs its stationary folding guiding system, matched to this cap size, for high-volume, single-SKU runs. Ask us about a servo-driven version if you need fast changeover across multiple cap sizes.
Quality and Performance
A folding machine is only as good as its reject rate. The FTC-100 targets a first-pass yield of 98%+ under standard operating conditions, meaning fewer than 2 in 100 caps need to be reworked or scrapped.
Add vision inspection and that number tightens further, since caps with an incomplete fold or misseated closure get pulled before they reach the collection box instead of shipping out with the good ones.
Most machines in this category don’t publish a number at all. We do, because it’s the number that actually tells you what a line will cost you in wasted caps over a production run.
98%+
Target First-Pass Yield
<2%
Reject Rate
Optional
Vision Inspection
100
Caps/Min Rated Output
What It's Compatible With
Cap Types Handled
Oval flip top caps
Round flip top caps
[Disc top caps, if applicable]
Materials
Polypropylene (PP)
[Other compatible polymers]
Typical Applications
Toothpaste & cream tubes
Cosmetics & personal care packaging
Pharmaceutical closures
Food & beverage caps
FTC-100 in Production
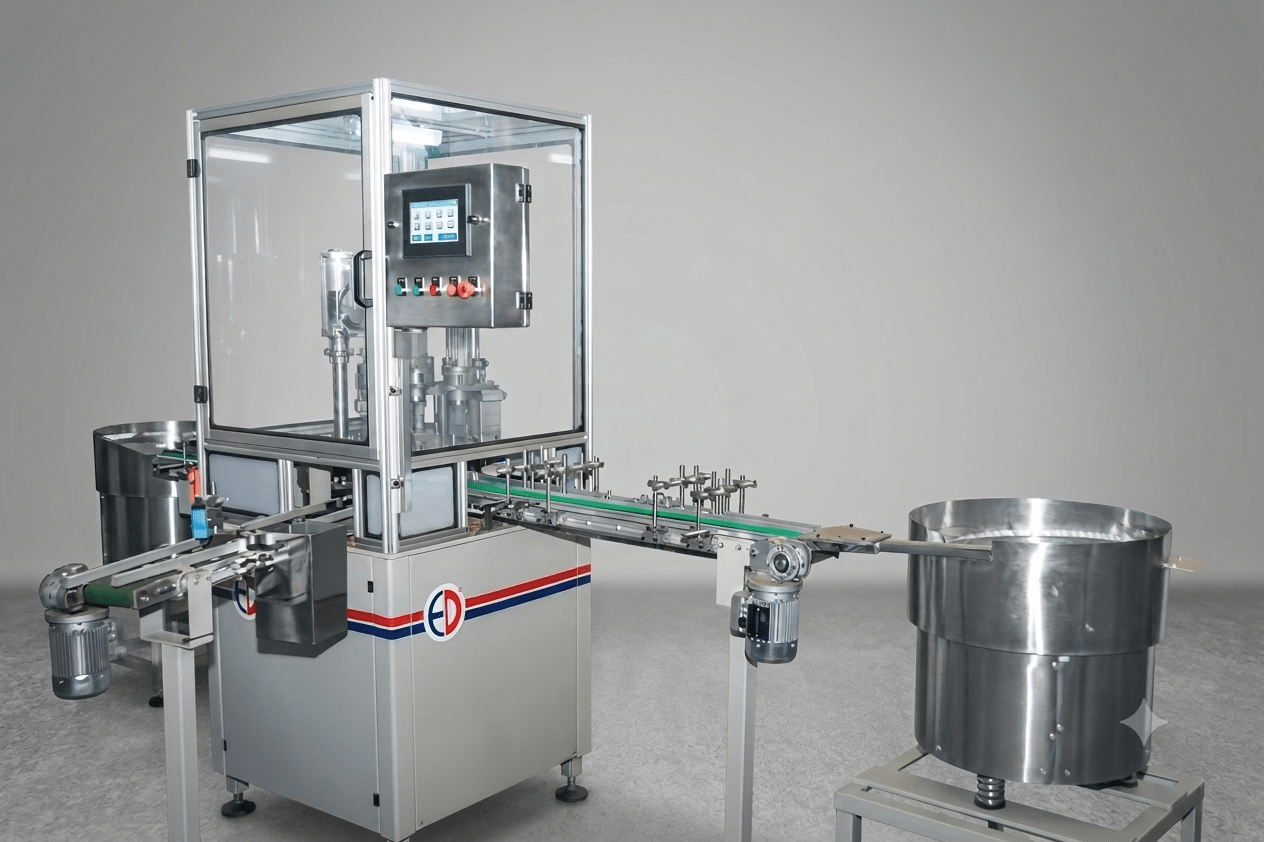
Full Machine View
SS 304 Vibratory Bowl Feeder
Star Wheel & Folding Guiding System
Roller & Pneumatic Cylinder
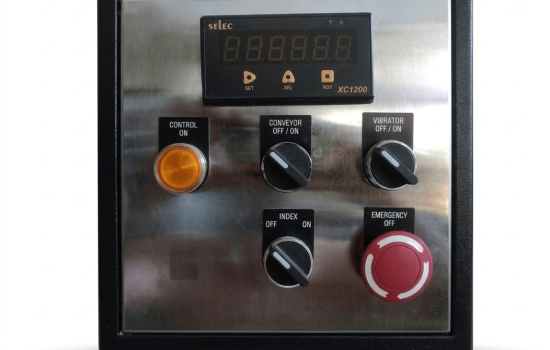
HMI / Control Panel
Ejection & Collection
Watch the FTC-100 Fold Oval Caps
Bowl feed, star wheel indexing, hinge heating, folding guiding system, and roller-and-cylinder locking, in one run on an oval cap.
The FTC-100 sits downstream from cap injection molding and upstream from your capping or filling line (see How It Works for the full sequence). Caps come in loose from molding, get folded and locked here, then move on to be applied to product.
[If PLC/IoT-enabled: the control system can report cycle counts and status back to your line monitoring.] Custom tooling is available to match your specific oval cap dimensions. An optional diverter can be added at additional cost to route rejected caps separately.
Sigma CapSeal designs, manufactures and supports reliable induction sealing and cap/closure automation systems that improve product safety, line efficiency, and packaging integrity for manufacturers across FMCG, pharmaceutical, personal care, chemicals, and food industries.
With more than five decades of domain expertise, hands-on R&D, and close partnerships with multinational customers, the FTC-100 reflects Sigma CapSeal’s commitment to solving the oval-cap problem properly instead of adapting a round-cap machine and calling it done.
Frequently Asked Questions: FTC 100
Common questions from cap manufacturers and packaging teams evaluating the FTC-100.
What is a flip top cap folding machine used for?
A flip top cap is a single molded piece with a built-in hinge, and it arrives from injection molding already open. The machine’s job is to close and lock that hinge, not join two separate cap components, so caps get folded shut and locked before they’re packed or sent to a capping line.
What is an oval flip top cap used for?
Oval caps are common on toothpaste, cream and other tube-style packaging, where the tube mouth itself is oval rather than round.
What cap sizes can it handle?
100 caps per minute under standard operating conditions.
Does the FTC-100 use a cam to fold the cap?
No. The cap is held in the star wheel pocket and moves in continuous rotary motion. The outer flip is heated, then closed by contact with a stationary folding guiding system as the cap rotates past it, not a cam-based design.
Is a diverter included?
Not as standard. A diverter mechanism to route rejected caps separately is available as an optional accessory at additional cost.
How does a cap folding machine work?
Caps are fed from an SS 304 vibratory bowl, oriented, carried by conveyor into a rotary star wheel, passed under a hot air heater to soften the hinge, folded by contact with a stationary folding guiding system, closed and locked by a silicon-based roller, given a final press by a pneumatic cylinder, then ejected into a collection box.
What's the difference between an oval and round cap folding machine?
An oval cap isn’t symmetric, so the bowl feeder tooling, star wheel pockets and folding guiding system all have to be built around its long and short axis. A machine set up only for round caps won’t fold ovals consistently.
What happens to caps that don't assemble correctly?
Any shape or diameter. Tooling is custom-matched to your cap, whether oval, round, or another profile.
Is the FTC-100 fully automatic?
Yes. Feeding, orientation, heating, folding, locking and ejection all run without manual handling.
What does a flip top cap folding machine cost?
Pricing depends on cap size range, output speed, and whether vision inspection or the optional diverter is included. Contact us with your cap specification for a quote.
Ready to Specify the FTC-100 for Your Line?
Talk to a Sigma CapSeal applications engineer. Bring your cap dimensions and target output, and we’ll confirm the right configuration and tooling.